Hey everyone, if you’ve ever hung around a metal fabrication shop long enough to hear the high-pitched whine of cold rolling equipment, you know it’s not just loud—it’s intense. As someone who’s been a cold rolling equipment supplier for over 12 years, I’ve spent way too many late nights troubleshooting why a customer’s line shut down mid-shift, and way too many early mornings talking through why their cooling system was the unsung hero of their whole operation. Today, let’s break down what that cooling system actually does, because way too many operators I meet treat it like an afterthought—until it’s the reason their entire production goes sideways. Cold Rolling Equipment
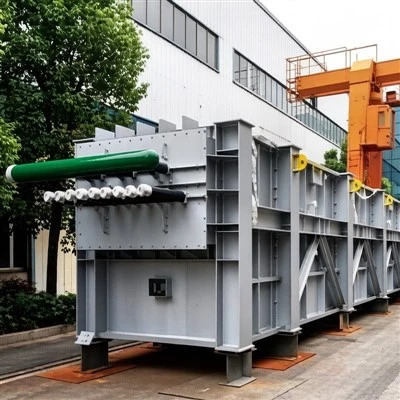
First off, let’s get one thing straight: cold rolling isn’t like hot rolling. Hot rolling uses super-heated metal, so heat is kind of part of the process, right? Cold rolling is done at room temp (or close to it) to make metal thinner, tighter, and way more consistent than hot rolled stock. But here’s the kicker—when the rolls squeeze the metal, friction is massive. Like, we’re talking temperatures that can spike to 200-300°C in a matter of minutes if you don’t do anything about it. That’s where the cooling system comes in, and it’s not just keeping things from melting. Let’s dive into the core roles, because there’s way more to it than just “lower the temp.”
First up: protecting the rolls themselves. Those rolls are precision-machined—we’re talking tolerances of a few microns, like 0.0001 inches, if you can wrap your head around that. If they get too hot, they expand. Even a tiny expansion throws off the entire thickness of the metal you’re rolling. I’ve seen a customer’s line that ran 100 tons of stainless steel suddenly start making sheets that were 0.002 inches off spec, and all it took was a clogged cooling nozzle that made one roll expand unevenly. They didn’t even notice the nozzle was blocked until we checked the cooling system, and that fix saved them from scrapping 50 tons of material. The cooling system keeps the rolls at a steady, consistent temp—usually around 40-50°C, depending on the material—so their shape stays perfect, every single pass.
Then there’s the metal itself. When you cold roll, you’re doing what’s called “work hardening” the metal. That’s a good thing, because it makes the metal stronger, harder, more durable—exactly what customers want for things like car body panels or aluminum cans. But if the metal gets too hot during rolling, that work hardening gets messed up. Too much heat, and the metal starts to soften a little, which ruins its mechanical properties. For example, if you’re rolling aluminum for beverage cans, the strength has to be exactly right to hold pressure without crumpling. One customer a few years back was rolling cans and getting constant leaks because their cooling system was underperforming—their aluminum sheets were too soft from excess heat, so they would bulge when filled. We upgraded their cooling setup, and their leak rate dropped by 85% overnight. The cooling system also prevents things like annealing, which is when metal starts to recrystallize and soften at high temps—total disaster for cold rolling quality.
Wait, another big one: reducing friction and wear. Think about rubbing your hands together fast—they get hot, right? That’s friction. When rolls rub against metal at 500+ feet per minute (we have lines that run up to 1,500 fpm now), friction is the enemy. The cooling system uses a mix of water and emulsion (usually oil and water, depending on the material) that acts as a lubricant, too. It’s not just cooling—this fluid fills the tiny gaps between the roll and the metal, cutting friction way down. Less friction means less wear on the rolls, which extends their life by years, not months. I had a customer who skipped proper cooling and went through a set of rolls every 6 months. After we set them up with a closed-loop cooling system that filtered the emulsion properly, they only change rolls every 3 years. That’s a huge cost savings—rolls for a cold rolling line aren’t cheap, like $20k+ per set for stainless steel. Friction also causes noise, too—operators hate the constant screech of metal grinding against hot rolls, so a good cooling system makes the shop a nicer, quieter place to work.
Now, let’s talk about process consistency. If your cooling system is all over the place—one minute the fluid is 45°C, the next it’s 55°C, or some rolls get more coolant than others—your output is going to be all over the map. Thickness variations, surface defects, mechanical property inconsistencies, all that garbage. We’ve had customers who would run the same job one day and get perfect sheets, then the next day get a bunch of scrap, and couldn’t figure out why. Half the time, it’s the cooling system’s temperature control being out of whack. Modern cooling systems use PLCs (programmable logic controllers, if you don’t know that term) that monitor temp in real time, adjust flow rates, even filter out tiny metal shavings that can clog nozzles. That consistency is what lets customers run lights-out production, too—they can walk away from the line and know it’s going to make good parts all shift long.
Oh, and surface quality! No one wants a metal sheet with scratches, discoloration, or residue that’s hard to get off. If the cooling system is working right, the coolant flushes away all the metal fines (tiny little metal particles) that get ground off during rolling, so they don’t get stuck between the roll and the metal. Those fines cause surface scratches that make the material unusable for things like appliance panels or automotive parts that need a smooth finish. We had a customer rolling galvanized steel for washing machine exteriors that was getting constant surface defects, and after we fixed their cooling nozzles and added a better filtration system, their defect rate for surface stuff went from 12% to less than 1%. That’s millions in scrap saved every year.
Wait, let’s not forget about uptime. If your cooling system fails, your whole cold rolling line stops. And time is money—each hour a line is down can cost tens of thousands of dollars, depending on the line’s output. I’ve seen a major auto parts manufacturer lose $150k in a single day because their cooling pump died, and they couldn’t get a replacement in time. A good cooling system isn’t just about keeping quality high—it’s about keeping production running. That’s why we always tell customers not to skimp on the cooling setup. A lot of guys come to us with a beat-up old line they bought used, and they only want to replace the rolls or the motors, but when we suggest upgrading the cooling system first, it’s the best decision they make.
Now, let’s get real about common mistakes I see customers making with their cooling systems. First, they under-size the system. They buy a line that’s rated for X tons of metal, but get a cooling system that’s only designed for half that, and wonder why it overheats. Second, they skip maintenance. Nozzles get clogged, filters get dirty, pumps wear out, and they don’t check it until something breaks. We tell every customer to do a weekly check: clean the nozzles, test the coolant temp, check for leaks, and change the filters every 3 months. Third, they use the wrong coolant. Some use straight water, which causes corrosion on the rolls and line parts, or use an emulsion with the wrong oil mix for their material. For example, stainless steel needs a different emulsion than aluminum—using the wrong one will cause more friction, more heat, and worse surface defects.
As a cold rolling equipment supplier, this is why we design our systems with the cooling front and center. We don’t just sell you a line that rolls metal—we integrate a cooling system that’s matched exactly to your line’s speed, material type, and output capacity. We use closed-loop systems that recycle coolant, so it’s not wasted, with PLC-controlled temp regulation and real-time monitoring. We even add filtration systems that catch tiny metal fines before they can clog nozzles or scratch the metal. And we don’t just sell it and leave—our techs train your operators on how to maintain the cooling system, because even the best system won’t work if no one knows how to use it right.
Look, I know a lot of operators and production managers see the cooling system as the “invisible workhorse” of their cold rolling line. It doesn’t get the hype that new rolls or faster motors do, but it’s the one thing that keeps quality high, costs low, and production moving. The next time your line is running smoothly, without scrap, without shutdowns, stop for 2 minutes and look at the pipes and nozzles spitting coolant on the rolls. That’s the cooling system doing its job, and doing it well.
If you’re looking to upgrade your cold rolling line, fix a persistent quality issue, or just make sure your cooling system is working as hard as it should be, hit us up to connect. We’ll walk through your setup, point out where you might be missing something, and help you get that unsung hero of your line working for you, not against you.
Heating Furnace References
- "Cold Rolling: Principles and Processes" by John S. Sokolowski, ASM International, 2006
- "Industrial Cooling Systems for Metal Fabrication" by the Metal Finishing Association, 2019
- "Advances in Cold Rolling Technology" by Elsevier, 2021
- "Quality Control in Cold Rolling Operations" by Society of Manufacturing Engineers, 2018
Jiangsu Dongfang Whole-Set Equipment Manufacturing Group Co., Ltd.
We are one of the most professional cold rolling equipment manufacturers and suppliers in China, also support customized service. With abundant experience, we warmly welcome you to buy durable cold rolling equipment from our factory. If you have any enquiry about pricelist, please feel free to email us.
Address: No. 9, Industrial Park, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: dfctwm@163.com
WebSite: https://www.dongfangequip.com/
